Selected engineering work

Engineering projects, delivered from concept to operation.

Project leadership, process and manufacturing engineering, continuous improvement, NPI, capital equipment and mechanical design across international industrial settings.

Engineering across international manufacturing settings

UK · Saudi Arabia · Pakistan | Technology sourcing & supplier collaboration: China · Germany
PEC Registered Engineer · Lean Six Sigma Green Belt · Associate Member, IMechE

Project leadership

Planning, supplier coordination, commissioning and workforce readiness.

Procurement & supply chain

Engineering-led technical sourcing, quotation evaluation, supplier negotiation, purchasing controls and equipment delivery.

Production Consumables & Tooling Cost Optimisation

UK Engineering Company, Tier 2 Automotive & Aircraft Parts Supplier | Production Engineer

Project type
Engineering-led materials and tooling selection for manufacturing process improvement, supported by supplier coordination.
My role
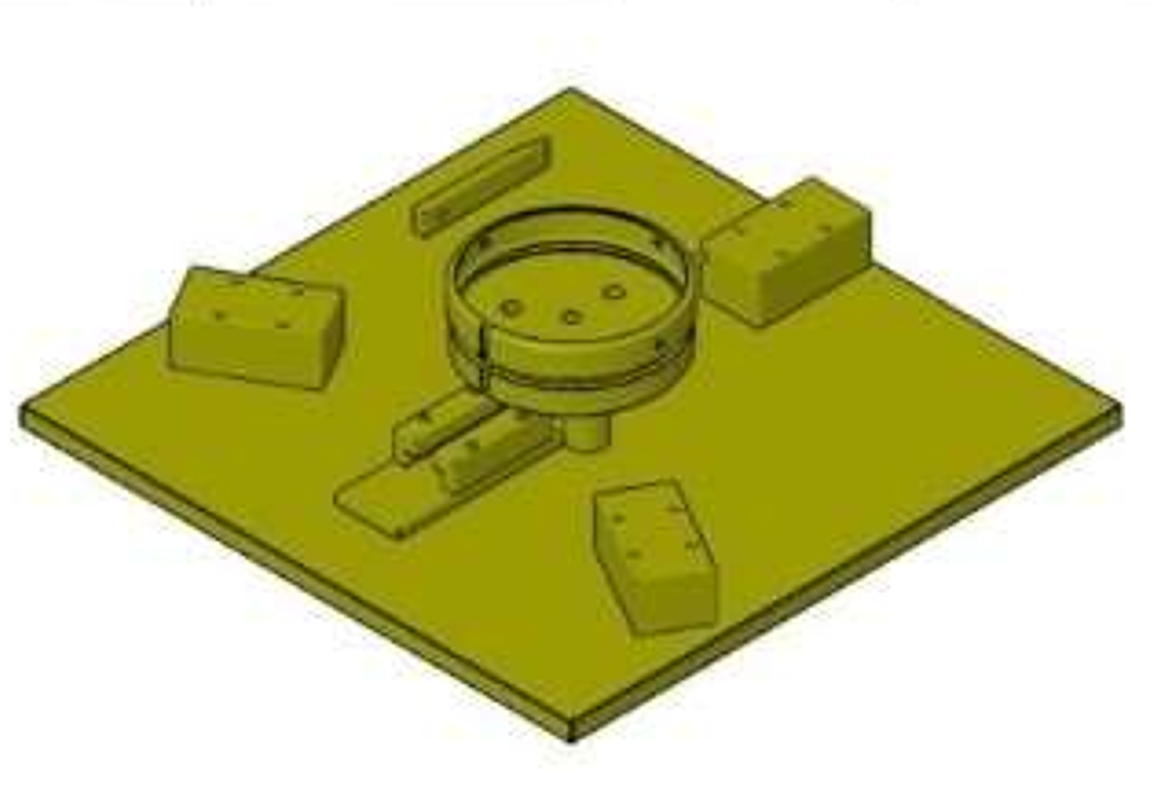
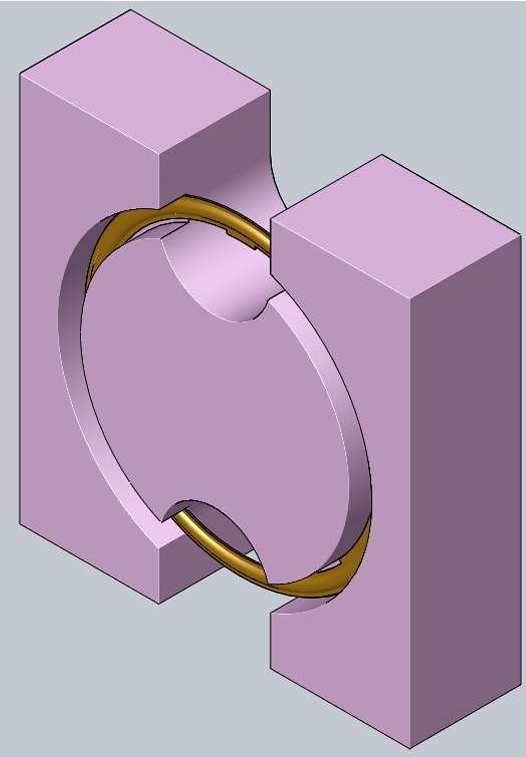
Investigated recurring cracking of rotary part-marking stamps and assessed material and tooling alternatives. Developed an improved stamp-holder design and revised the material selection to reduce consumables usage and cost. Coordinated technical requirements and implementation of the revised tooling.
Techniques
Tooling specification, alternative-material assessment, engineering cost analysis, design improvement, trials and implementation.
End result
Redesigned the rotary part-marking stamp solution, achieving an 80% reduction in consumables cost after implementation. The cost reduction arose from engineering redesign and implementation; it is not presented as an 80% supplier-price discount.

CNC Composite Veil Cutting — Tooling Procurement & Monitoring

UK Composite Manufacturing Company | Process Engineer (Contract)

Project type
Tooling procurement, equipment reliability and production-monitoring improvements for a specialist CNC composite-veil cutting line.
My role
Supported tooling and supplier coordination for an automated cutting and collection process producing narrower finished veil rolls, typically seven or eight rolls from a parent coil. Negotiated a 15% reduction against a supplier’s quoted price. Worked with a contractor on embedded software to report breakdowns, machine efficiency, job name/type and operator identification.
Techniques
Technical tooling review, commercial negotiation, supplier and contractor coordination, monitoring-system requirements, OEE analysis and operational improvement.
End result
Achieved a 15% negotiated reduction from the quoted price. The overall project delivered approximately £30,000 in benefits from a combination of procurement savings, lower breakdown-related losses, higher machine efficiency and reduced non-compliance; the £30,000 is not presented as a procurement-only saving.

German CNC Fin Machine & UK Boxing Station Procurement

UK Manufacturing Company & Tier 1 Automotive Supplier | Machine Development Engineer (Advanced Specialist)

Project type
Technical acquisition and supplier negotiation for CNC fin-forming technology and an integrated automated parts-collection station.
My role
Specified and coordinated procurement of an automated CNC fin manufacturing machine from a German supplier and an integrated boxing station from a UK supplier. Assessed functional and operating requirements, negotiated equipment pricing, raised purchase orders for engineering projects, monitored supplier approvals and deliveries, and supported commissioning and supplier-payment checks.
Techniques
International and UK supplier sourcing, technical specification, negotiation, purchase orders, delivery coordination, PO/GRN/invoice three-way matching, RAMS and commissioning.
End result
Negotiated a 12% reduction on the German CNC machine and a separate 3% reduction on the UK boxing station, while supporting equipment introduction and technical commissioning. These percentages are separate supplier reductions and have not been added together.

D2 Raw Material, Chemical & Paint Procurement Optimisation

UK Engineering Company | Process Engineer

Project type
Raw-material and process-chemical purchasing optimisation, together with a separate paint-material improvement initiative.
My role
Reviewed procurement costs and purchasing arrangements for D2 steel billets and chemicals associated with the seven-stage chemical blackening process. Negotiated price reductions and price-stability terms with the principal supplier and established automated stock-level alerts to support timely replenishment. Also investigated paint requirements and improved paint selection and process controls as a separate initiative.
Techniques
Supplier negotiation, purchasing-cost analysis, material and chemical specifications, price-stability arrangements, inventory thresholds, replenishment alerts, supplier consultation and process controls.
End result
Reduced combined D2 raw-material billet and blackening-chemical costs by approximately £27,000 per year. Separately, the paint improvement delivered approximately £7,500 annual savings, and the process-quality blackening case study records £18,000 annual scrapped-part replacement savings. These different cost bases are not combined into a single total.

Engineering projects

Selected examples of project scope, individual contribution, methods and measurable results.

NPI and manufacturing readiness

Project type
Introduction of new production equipment.
My role
Led engineering work from equipment introduction through production readiness.
Techniques
Process planning, risk identification, mitigation and transfer, cross-functional coordination and KPI tracking.
End result
Met 100% of project KPIs and eliminated or transferred 70% of identified open risks.

Automotive NPI and process capability

Project type
High-volume automotive component introduction for a Tier 1 supplier.
My role
Worked from feasibility and manufacturing cost assessment through tooling design, manufacture and development; recommended a material specification change based on engineering calculations, then led process validation and production handover.
Techniques
Manufacturing and tooling cost analysis, engineering calculations, tooling development, PPAP, statistical process capability analysis in Minitab, FMEA, control planning, work instructions and staff training.
End result
Centred the process and secured approval after capability studies across selected profile and dimensional characteristics; the lowest achieved Cpk was 1.73, with most results around 2.0. Prepared production staff with documented controls and training.

Versatile metal-forming capability

Project type
NPI manufacturing capability and capital cost reduction.
My role
Conceived and developed versatile tooling, adapted an existing machine and commissioned the resulting manufacturing process.
Techniques
Tooling design, machine modification, process trials, PPAP approval and operator training.
End result
Enabled production of several product shapes to the required quality and avoided purchase of four dedicated machines. Achieved £350,000 in net NPI savings after tooling and machine modification costs.

Rebuild Machine Authorisation workflow

Full process lead time per RMA project
Before299 h
After79 h

Rounded values shown; underlying analysis: 298.58 → 79.45 hours.

Project type
RMA document processing improvement
My role
Led the project through the DMAIC stages, from analysing delays to implementing and controlling the revised process.
Techniques
SIPOC, Pareto analysis, value stream mapping, measurement and capability analysis, root-cause and hypothesis testing, FMEA, cost analysis and a revised standard operating procedure.
End result
After implementation, measured a reduction in full process lead time of approximately 219 hours (73.4%) per completed RMA project, with approximately £12,000 saved per project based on a full cost analysis.

Cropping die improvement

Project type
Continuous improvement of production tooling.
My role
Developed and implemented a cropping die improvement.
Techniques
Root-cause analysis, tooling review and production trials.
End result
Measured a 10% productivity increase and a 25% reduction in component cost after implementation.

Automated material feeding improvement

Project type
Quality improvement for an automated metal-forming process.
My role
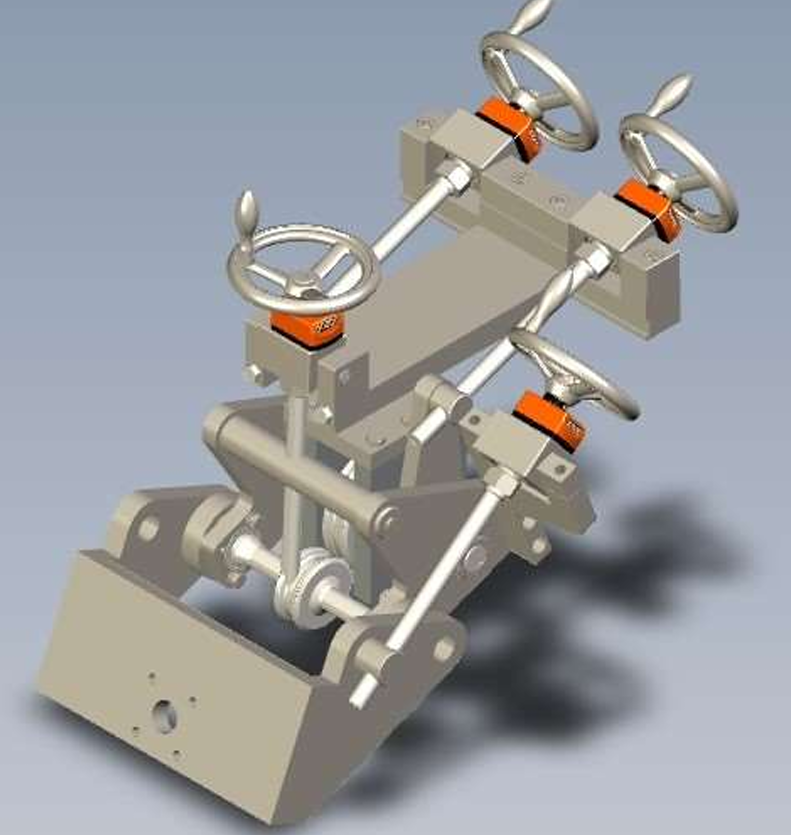
Led the 8D investigation, redesigned the automated material feeding system, removed the existing system and installed and commissioned its replacement.
Techniques
8D problem solving, root-cause analysis, mechanical design and commissioning.
End result
Confirmed the quality issue was resolved in production, with £76,000 in projected annual savings including reduced setup scrap. Lower downtime labour and nonconformance costs were additional, unquantified benefits.

Capital equipment sourcing and development

Project type
Continuous improvement and CAPEX.
My role
Led supplier selection, negotiation, engineering design support, commissioning and delivery to sites in the UK, Mexico and Poland.
Techniques
Supplier development, CAD design, roll-bending engineering and project management.
End result
Delivered five machines sourced from China for a total of £125,000, including shipping, installation and commissioning, compared with the lowest UK supplier quotation of £450,000 for the equivalent scope. Achieved an exact £325,000 one-time procurement saving.

Seven-stage chemical blackening process improvement

Project type
Process engineering and quality improvement.
My role
Investigated part rejections, consulted suppliers and developed material-specific procedures, work instructions and a defect catalogue.
Techniques
Process research, supplier consultation, procedure development and incoming and outgoing inspection criteria.
End result
After adopting the revised procedures, reduced part rejection and achieved £18,000 in annual scrapped-part replacement savings. Nonconformance handling and manufacturing delay costs were excluded.

Composite veil production reliability

Project type
TPM and reliability improvement for CNC composite veil manufacturing equipment.
My role
Analysed daily MES/OEE reports, prioritised causes of line stoppages and coordinated production, maintenance and suppliers through modifications, commissioning, procedures and training.
Techniques
OEE analysis, cross-functional problem solving, supplier coordination, commissioning and SOP development.
End result
Resolved recurring equipment issues and measured a 70% reduction in breakdowns in the first month after the modifications.

Mechanical design

Design and design-review work across equipment, mechanisms, tooling and assembly.

Rotary part-marking equipment

Project type
Production equipment redesign
My role
Redesigned a rotary part-marking solution.
Techniques
Mechanical design, equipment review and production trials.
End result
Reduced consumables cost by 80%, measured after the redesigned system was put into use.

CNC machine assembly planning

Project type
In-house machine manufacturing and assembly planning.
My role
Checked machine designs and planned the assembly flow for equipment built in-house by a manufacturer of machines and parts.
Techniques
NX12, design checks, assembly-flow planning and factory-layout work.
End result
Delivered an approved layout that made machine builds easier and improved the assembly workflow.

Approach

From an operational need to an implemented engineering solution.

Identify the need · assess technical and delivery risks · work across engineering, production, quality and suppliers · verify the result in operation.